Choosing the right Rubber Tire Shredder in 2026 requires more than comparing motor power and purchase prices. Tire composition, feed size, output requirements, and daily operating hours all influence performance. A machine handling passenger tires may struggle with truck tires or reinforced sidewalls. That difference matters.
A practical evaluation should examine cutting chamber design, knife quality, drive protection, dust control, noise levels, and emergency stopping systems. Ask for verified throughput data under conditions similar to your facility. Manufacturer figures can look impressive. Real production may be lower when tires contain steel, moisture, or irregular shapes. Inspect the hopper, conveyor, and discharge area if possible. These details reveal more than polished brochures. Service access is also important. Technicians should reach knives, bearings, and screens without excessive downtime. Reliable suppliers provide clear manuals, parts support, training, and documented safety procedures.
No machine wins everywhere. A lower-priced shredder may consume more energy or require frequent knife changes. A powerful model may be wasteful for a small operation. I have seen buyers focus on capacity while overlooking maintenance space and electrical requirements. That mistake becomes expensive. The best choice balances throughput, durability, safety, operating cost, and future expansion. It should also support responsible recycling practices and comply with applicable workplace and environmental requirements. Before signing a purchase agreement, compare test results, warranty terms, references, and total ownership costs. Leave room for doubt. A careful decision is usually stronger than a rushed one.
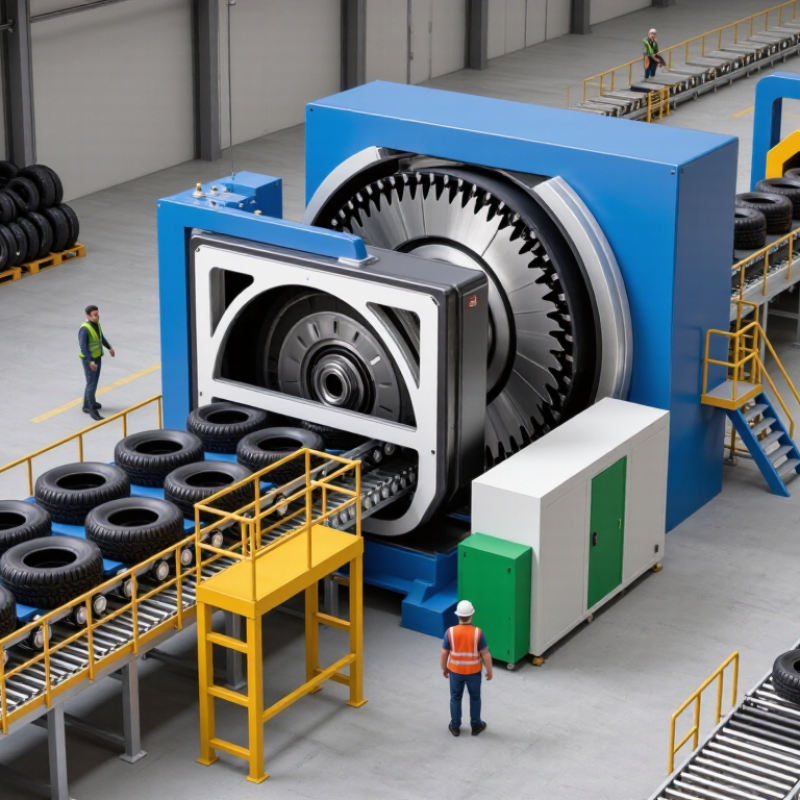
How to Choose the Best Rubber Tire Shredder in 2026?
The EPA reports about 290 million scrap tires are generated annually in the United States. This figure makes feedstock definition essential before selecting a rubber tire shredder. Passenger tires, truck tires, and oversized tires require different cutting forces. Steel content also changes wear rates and energy demand.
In practical shredder evaluations, operators should record tire sizes, daily volume, moisture, and contamination. A machine designed for passenger tires may struggle with thick commercial casings. Ask for verified throughput data under similar conditions. Check whether the stated capacity includes clean tires or mixed feedstock. That detail is easy to miss. It can distort the entire budget.
Tips: Inspect knife design, screen access, bearing protection, and emergency controls. Confirm how quickly worn parts can be replaced. Request maintenance records from comparable operations when possible. Output size matters too. Coarse rubber may suit fuel preparation, while smaller particles support further processing. Local environmental and workplace requirements should guide installation and operation. A perfect calculation is rare, so allow space for seasonal volume changes and unexpected contamination.
The global 1.5 billion end-of-life tire stream creates a serious capacity question. The World Business Council for Sustainable Development reports that about 1.5 billion tires reach end of life globally each year. That figure is not a machine specification. It is a planning warning. Your shredder must match local supply, operating hours, and realistic uptime.
Start with tonnes per hour, not brochure claims. A facility receiving 80 tonnes daily may need a 10-tonne-per-hour system across two shifts. However, wet tires, steel content, loading delays, and maintenance can reduce actual output. Leave room for error. A practical target may be 15–25% above average demand. That margin feels expensive, but missed production is usually worse.
The European Tyre and Rubber Manufacturers’ Association reported approximately 3.9 million tonnes of end-of-life tires in Europe during 2021. Its recovery data also shows how established processing networks can absorb large volumes. When comparing shredders, inspect particle size, tire diameter limits, knife life, energy use, and safe access for maintenance. Ask for independently measured throughput under similar feed conditions. Not laboratory numbers. Also review dust control and noise performance, because operators experience those details every shift. A perfect capacity model rarely survives the first month. Recheck it.
How to Choose the Best Rubber Tire Shredder in 2026?
Choosing a rubber tire shredder starts with the required tire-derived fuel chip size. For 1–3 inch chips, cutter geometry matters more than advertised motor power. A twin-shaft cutter with hooked, hardened blades usually handles passenger and truck tires effectively. Its slower cutting action creates strong torque and reduces sudden overloads. However, blade spacing must match the target output. Wide spacing may produce oversized pieces, while narrow spacing can increase energy use and wear.
A practical system should include a sizing screen or controlled discharge opening. The screen holds back pieces that exceed the selected dimension. This improves fuel consistency for storage, feeding, and combustion systems. Measure actual chip samples from several batches. Do not judge performance from one clean tire. Steel belts, mud, moisture, and uneven sidewalls can change the result. A 2-inch setting may still produce occasional longer pieces.
Check the cutter chamber, bearing protection, and access for blade replacement. These details affect real operating costs. Torque monitoring also helps identify jams before serious damage occurs. In field evaluations, operators should record throughput, power consumption, chip size, and blade wear together. Focusing only on tons per hour can be misleading. I would also leave room for adjustment, because tire composition changes more than expected. The best design is not always the fastest one. It is the one that repeatedly delivers usable 1–3 inch chips without excessive maintenance.
Technical selection guide for producing nominal 1–3 inch tire-derived fuel (TDF) chips
| Application Target | Recommended Cutter Design | Typical Nominal Output | Recommended Sizing Method | Typical Feedstock | Indicative Throughput Range | Indicative Installed Power | Wire and Textile Handling | Best-Fit Operating Situation | Key Selection Check |
|---|---|---|---|---|---|---|---|---|---|
| Coarse 3-inch TDF chips | Low-speed, high-torque dual-shaft rotary shear with replaceable cutters | 2–4 inches; commonly specified as a nominal 3-inch product | Primary cutter gap and hook geometry; use a sizing screen only when tighter control is required | Passenger tires, light-truck tires, and whole tires with limited oversize content | Approximately 3–10 metric tonnes per hour, depending on tire size, feed method, and cutter width | Approximately 150–300 kW total drive power | Handles steel bead and belt wire, but downstream magnetic separation is normally required | High-volume TDF production where moderate size uniformity is acceptable | Confirm cutter torque, chamber opening, and automatic reverse protection against wire jams |
| Controlled 2-inch TDF chips | Primary rotary shear followed by a secondary single-shaft or counter-rotating cutter | 1.5–2.5 inches; nominal 2-inch product | Secondary sizing screen or calibrated cutter clearance | Passenger and truck tires after primary reduction | Approximately 2–8 metric tonnes per hour in a two-stage line | Approximately 200–400 kW combined system power | Use over-band or cross-belt magnetic separation between stages and after final sizing | Fuel users requiring more consistent chip dimensions and reduced oversize recirculation | Check the balance between screen area, rotor speed, recirculation rate, and heat generation |
| Fine 1-inch TDF chips | Two-stage system with a primary shear and a high-torque secondary granulator or fine cutter | 0.75–1.25 inches; nominal 1-inch product | Heavy-duty sizing screen with controlled rotor-to-screen clearance | Pre-shredded passenger and truck tire chips, generally below 3–4 inches | Approximately 1–5 metric tonnes per hour, depending on wire content and screen specification | Approximately 250–500 kW combined system power | Magnetic separation is essential; fine sizing increases the need to manage exposed steel wire | Applications with strict fuel-feed or combustion-system size limits | Verify screen wear resistance, access for cleaning, and protection from tramp metal |
| Mixed 1–3 inch TDF range | Variable-gap dual-shaft primary shredder with a secondary sizing stage and adjustable screen | 1–3 inches with controlled oversize recirculation | Interchangeable screens or adjustable secondary cutter settings | Mixed passenger, truck, and occasional off-the-road tires | Approximately 2–8 metric tonnes per hour for a properly matched two-stage line | Approximately 200–450 kW combined system power | Use staged magnetic separation and inspect residual wire in the finished fuel | Facilities serving multiple fuel specifications or changing buyer requirements | Choose a design that allows fast screen and cutter changes without major frame modification |
| Truck-tire-dominant feed | Wide-chamber, low-speed, high-torque shear with reinforced bearings and drive train | 2–4 inches after primary reduction; secondary sizing may produce 1–3 inches | Primary gap control followed by a secondary screen when required | Commercial truck tires, bus tires, and heavy sidewalls | Approximately 2–7 metric tonnes per hour, highly dependent on sidewall thickness and loading | Approximately 250–500 kW total system power | High steel content requires robust magnets and accessible wire-cleaning points | Operations processing large tires continuously rather than occasional mixed loads | Prioritize chamber opening, torque reserve, bearing protection, and tire-feeding equipment |
| Off-the-road or oversized tires | Heavy-duty primary shear with pre-cutting, guillotine preparation, or staged feeding | 3–6 inches from primary reduction; a further secondary stage is normally needed for 1–3 inches | Staged reduction with a dedicated secondary sizing machine | Earthmover, agricultural, mining, and other large-diameter tires | Approximately 1–5 metric tonnes per hour, depending on tire diameter and pre-processing | Approximately 350–700 kW for the complete staged system | Very high steel content may require multiple magnetic separators and manual quality checks | Specialized facilities handling large or heavily reinforced tires | Confirm maximum tire diameter, bead-cutting requirements, hydraulic pressure, and maintenance access |
| Low-maintenance, variable-volume operation | Slow-speed dual-shaft shear with automatic overload reversal and modular cutter stacks | Approximately 2–4 inches; final size depends on cutter spacing and feed control | Primary cutter geometry; add a secondary stage if a strict 1–3 inch specification is required | Intermittent mixed tire loads with variable steel and textile content | Approximately 1–6 metric tonnes per hour | Approximately 100–300 kW for primary shredding | Good tolerance for wire and textiles, but metal separation remains necessary | Smaller recycling sites prioritizing uptime and simple operation | Evaluate knife life, reverse-cycle controls, spare-cutter access, and hydraulic or electric drive serviceability |
Important: Throughput, power, and chip size are planning ranges rather than guaranteed performance figures. Actual results vary with tire diameter, rubber hardness, steel content, moisture, feed consistency, cutter wear, screen opening, and operating conditions.
Size definition: “1–3 inch” refers to nominal TDF chip dimensions. A purchaser should specify the maximum permitted oversize, fines percentage, and acceptable residual steel content separately.
Practical recommendation: A primary shredder is generally suitable for coarse TDF production. Consistent 1-inch or tightly controlled 2-inch material normally requires a secondary sizing stage, magnetic separation, and a defined quality-control procedure.
How to Choose the Best Rubber Tire Shredder in 2026?
Throughput should be measured with the tire type you actually process. Passenger tires, truck tires, and steel-heavy casings behave differently. Run a controlled test with one metric ton of prepared tires, then record output weight, operating time, stoppages, and particle size. Do not trust peak capacity alone. An imperfect test is still useful.
Motor power needs context. A 250 kW motor may handle difficult tires, but it can waste electricity during light loading. The U.S. Department of Energy reports that motor-driven systems use about 69% of industrial electricity, making efficient operation a serious purchasing factor. Install a power meter and calculate energy per ton: total kilowatt-hours divided by accepted output. For example, 190 kWh used to produce 4.5 tons equals 42.2 kWh per ton. That figure is more meaningful than motor size.
The Global Rubber Study Group’s World Rubber Industry Outlook 2024 highlights continuing growth in tire demand and material consumption, increasing pressure on recycling capacity. Compare at least three machines under identical conditions. Record feed moisture, blade condition, conveyor load, and screen settings. Small changes can distort results. A 15% higher throughput may look attractive, but not if energy rises by 40%. I would also repeat the test after several operating hours, because heat, wear, and blade dulling can change performance. Performance on day one is not the whole purchase decision.
Comparison of throughput, installed motor power, and energy consumption under controlled full-load test conditions.
Higher throughput does not automatically mean lower operating cost. The medium-capacity configuration delivered the lowest energy consumption at 90 kWh per ton, while the heavy-duty configuration achieved the highest throughput with a similar energy requirement per ton. Actual results vary with tire size, wire content, moisture, screen size, and maintenance condition.
Choosing a rubber tire shredder in 2026 requires more than checking throughput and motor power. OSHA’s FY2024 enforcement data placed machine guarding among its Top 10 frequently cited standards. That signal matters. Inspect the hopper, conveyor transfer points, rotor chamber, and discharge opening in person. Guards should prevent reach-in access, not merely look sturdy. I would not trust a polished enclosure alone.
Ask for the machine’s risk assessment and CE Declaration of Conformity. CE marking is not a quality award or an automatic OSHA approval. It indicates claimed conformity with applicable European requirements. Check whether the declaration matches the exact model, electrical design, and guarding arrangement. Also review emergency stops, trapped-key access, interlocked doors, and safe isolation points. ISO 13849-1:2023 requires safety-related control systems to achieve a risk-based Performance Level. The supplier should identify the required PLr, achieved PL, diagnostic coverage, and validation evidence.
Watch the rotor’s stopping time. A door that opens before the rotor stops can defeat every warning label. Test the interlock under realistic conditions, including power loss and restart attempts. OSHA’s lockout/tagout standard, 29 CFR 1910.147, remains essential during clearing and maintenance. I still find this easy to overlook during a factory tour. Ask who tested the safety circuit, with which instrument, and when. Missing records are not proof of failure, but they deserve careful questioning.